ISO 14373:2015 PDF
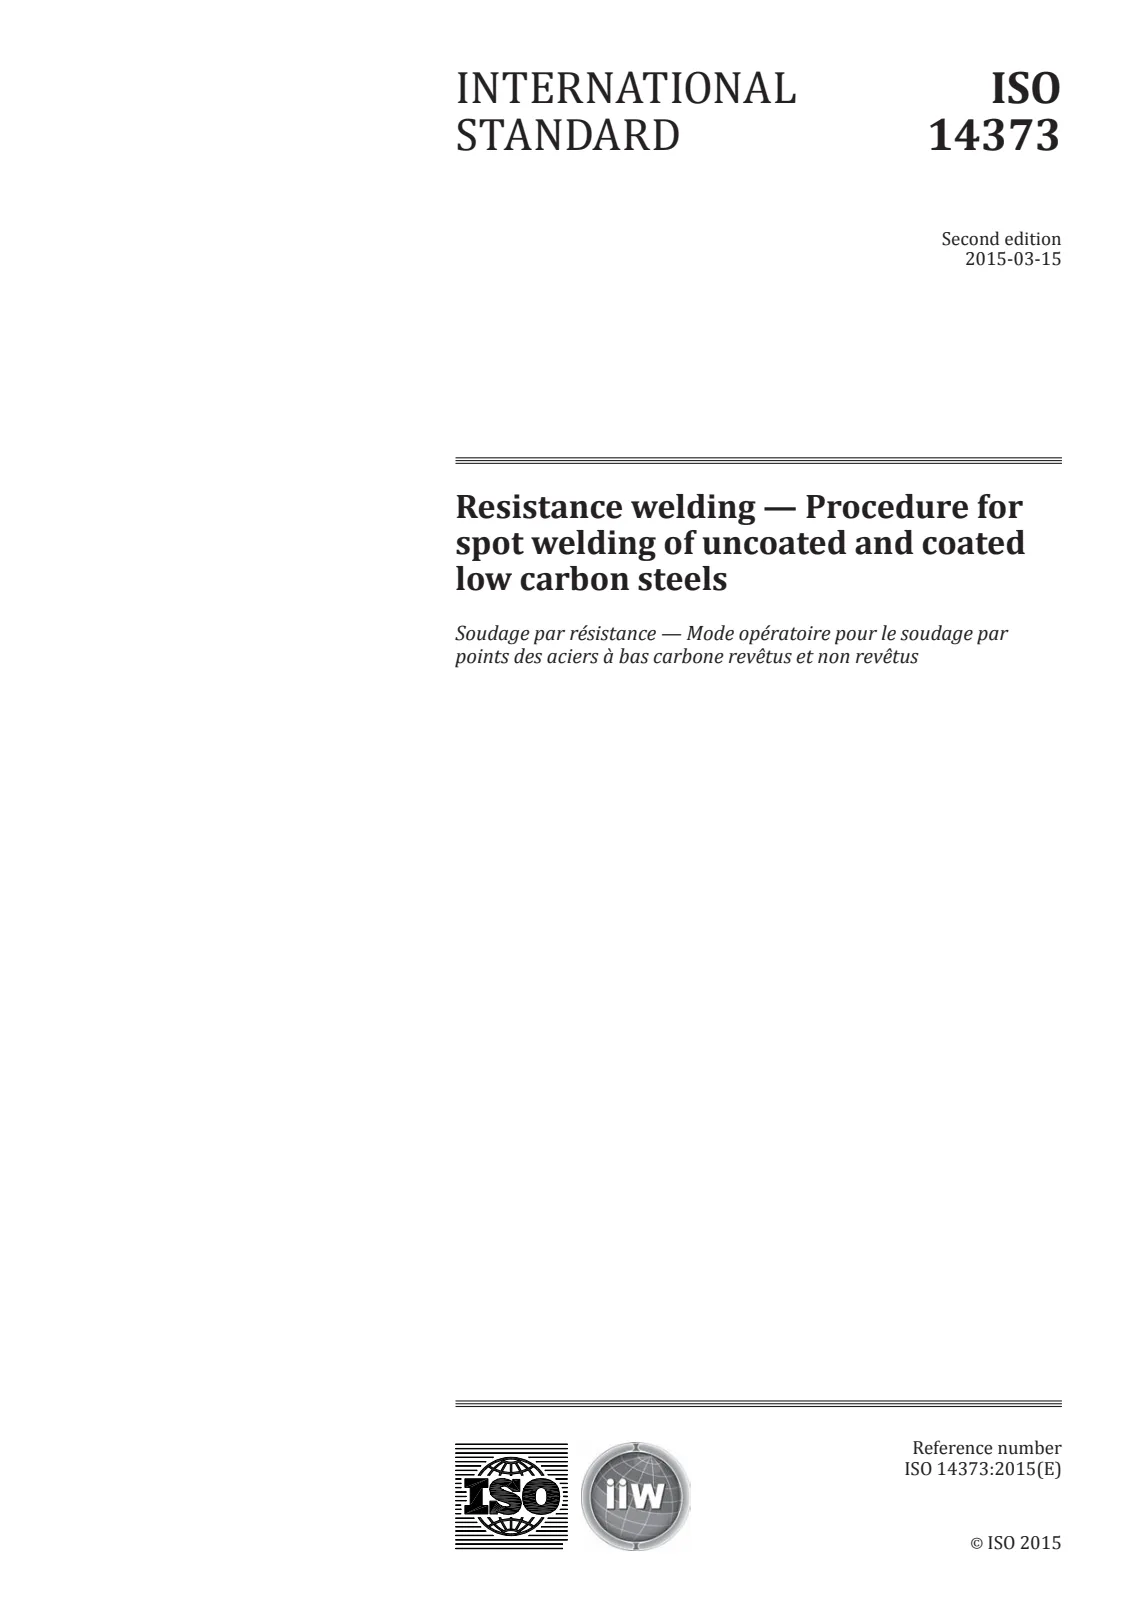
Resistance welding — Procedure for spot welding of uncoated and coated low carbon steels
 Open preview (PDF)Resistance welding — Procedure for spot welding of uncoated and coated low carbon steels
Resistance welding — Procedure for spot welding of uncoated and coated low carbon steels
- Document status:
- Withdrawn
- Format:
- Electronic (PDF)
- Number of pages:
- 15
- Publication date:
- March 13, 2015
- Edition:
- ISO IS 14373 edition 2 version 1
- ICS:
- 25.160.10
ISO 14373:2015 specifies requirements for resistance spot welding in the fabrication of assemblies of uncoated and metallic coated low carbon steel, comprising two or three sheets of metal, where the maximum single sheet thickness of components to be welded is within the range 0,4 mm to 3 mm, for the following materials: uncoated steels; hot-dip zinc or iron-zinc alloy (galvannealed) coated steel; electrolytic zinc, zinc-iron, or zinc-nickel coated steel; aluminium coated steel; zinc-aluminium coated steel. It is applicable to welding of sheets of the same or dissimilar thickness, where the thickness ratio is less than or equal to 3:1. It applies to the welding of three thicknesses, where the total thickness is less than or equal to 9 mm. Welding with the following types of equipment is within its scope: pedestal welding equipment; gun welders; automatic welding equipment where the components are fed by robots or automatic feeding equipment; multi welders; robotic welders. It also gives information, for guidance only, on appropriate welding equipment on spot welding conditions. The welding of organic coated or primer coated steels is not within its scope.
Technical details
- Technical committee
- ISO/TC 44/SC 6 - Resistance welding and allied mechanical joining
- SKU
- ISO 14373:2015